CNC Turret Punching · Miami Gardens, Florida
CNC Punching Services
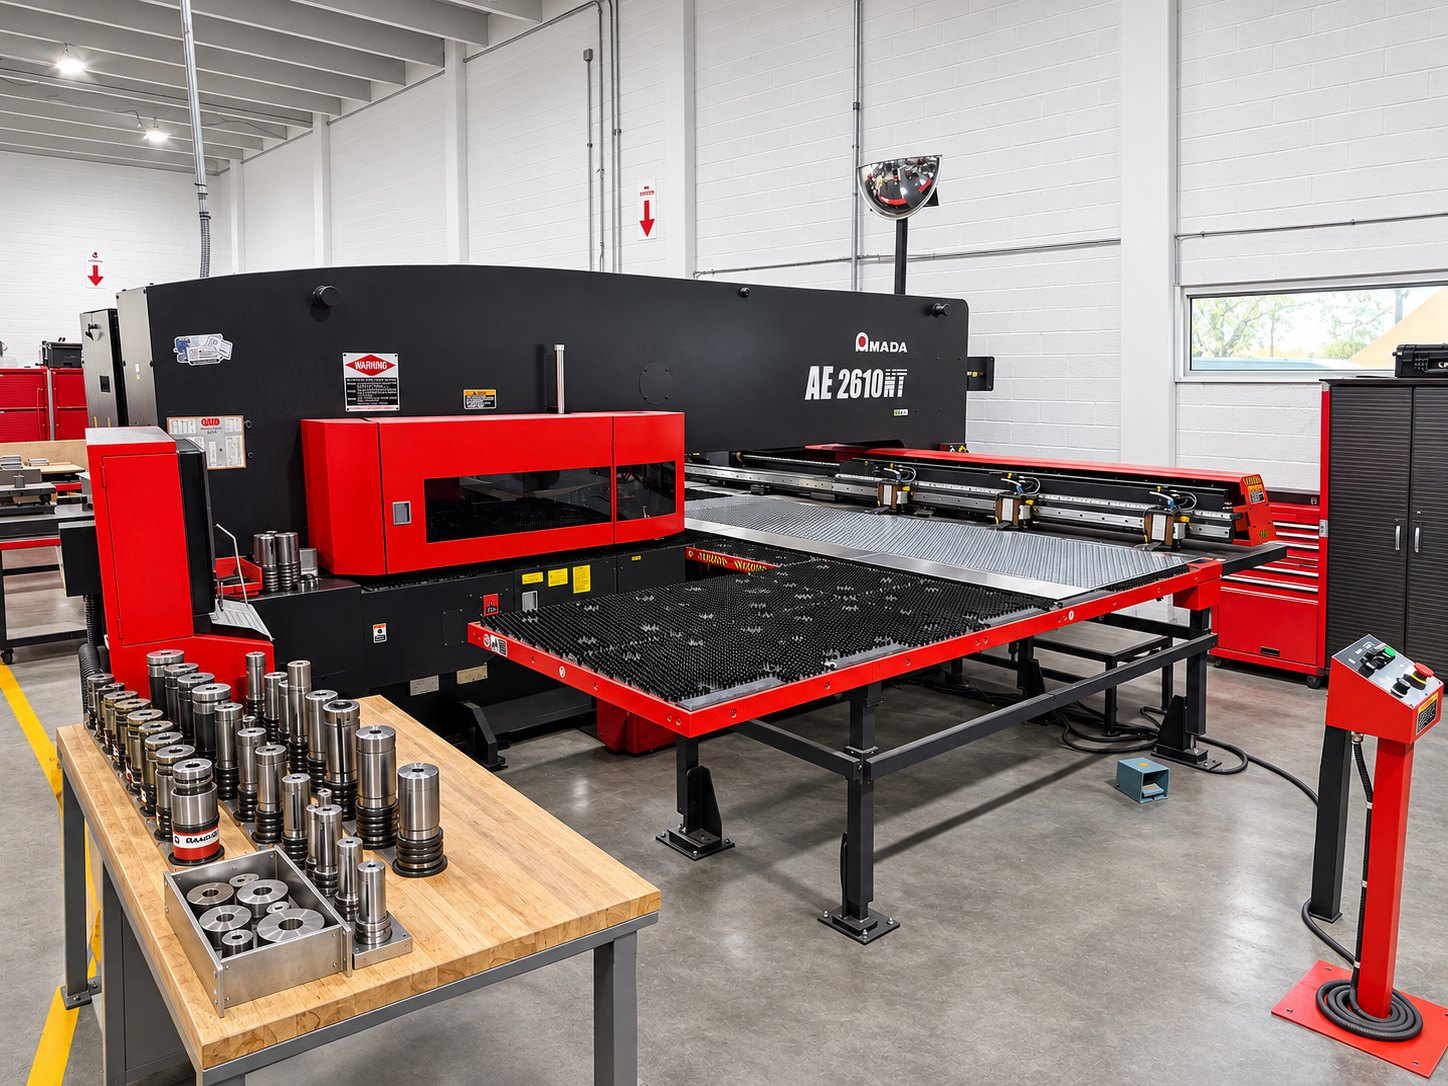
Our Amada AE 2610NT CNC turret punch produces holes, louvers, embosses, extrusions, lances and knockouts in a single setup, backed by a library of 794 standard and special tools. For parts with many repeated features or formed details, punching beats laser cutting on cost.
Overview
When a Turret Punch Is the Right Tool
A laser cuts any shape but only cuts. A turret punch also forms. Louvers, countersinks, embosses, extruded holes for tapping, card guides and electrical knockouts are made in the flat on the punch, in the same hit sequence as the holes, with no second operation. On perforated panels and parts with hundreds of identical holes, the punch is also faster.
We run both processes side by side, with five Amada lasers next to the turret, so each part goes to whichever is cheaper and better for it. Often that is a combination. See laser cutting vs CNC punching.
Specifications
Turret Punching Capabilities
| Specification | Detail |
|---|---|
| Machine | Amada AE 2610NT CNC turret punch press |
| Thickness | Mild steel and aluminum up to 0.250 in. (1/4 in.) |
| Typical tolerance | ±0.005 in. |
| Operations | Punching, perforating, nibbling, blanking, forming, embossing, louvering, lancing, extruding and knockouts |
| Materials | Mild steel, stainless steel, aluminum, galvanized, galvanneal, copper, brass, titanium, polycarbonate and other non-metallic sheet |
| Tooling | 794 standard and special tools. Browse every size and shape, with drawings, in the Turret Punch Tool Library |
Features
Features We Punch and Form
Round, square, rectangular, obround and special-shape holes; vent patterns and perforated panels.
Ventilation louvers formed in the flat with consistent height and spacing.
Stiffening embosses, offsets, standoff dimples and countersink forms for flush screws.
Extruded holes that give thin sheet enough thread depth to be tapped.
Card guides, cable tie bridges, tabs and locating features.
Electrical knockouts for enclosures and junction boxes.
If your drawing calls for a shape that is not in our tool library, send it. Special tools can be ordered when the volume justifies it, or we will cut the feature on a laser.
Design Notes
Designing Parts for Punching
- Use tools we already own. Matching your hole sizes, louvers and knockouts to the tool library avoids tooling cost and lead time.
- Keep holes at least one material thickness in diameter, and keep features away from edges and bends so they do not distort.
- Formed features have a direction. Show which side louvers and embosses face, and leave room for the tool body around them.
- Tell us the annual volume. It decides whether punching, laser cutting or a mix gives the lowest piece price.
See the DFM guide and tolerances.
After Punching
Punched Parts, Finished
Punched blanks move straight to deburring on three Timesavers wet machines, then forming on nine Amada press brakes, hardware insertion, welding, finishing and inspection. Flat parts are checked on our Amada Fabri-Vision optical inspection system against the CAD file.
Straight Talk
Where Punching Does Not Win
Thick plate, complex outside contours, very small quantities with no repeated features, and cosmetic edges with no nibble marks are laser jobs. Material over 1/4 in. does not go on the turret at all.
You do not have to decide. Send the part and we will quote the process that makes it best.
FAQ
CNC Punching Questions
What CNC punching equipment does MJM have?
MJM operates an Amada AE 2610NT CNC turret punch press with a library of 794 standard and special tools, at its Miami Gardens, Florida facility.
How thick can MJM punch?
Up to 0.250 in. (1/4 in.) in mild steel and aluminum, at a typical tolerance of ±0.005 in.
Is CNC punching cheaper than laser cutting?
For parts with many repeated holes, perforations or formed features such as louvers and embosses, punching is usually cheaper and faster. For complex contours, thick material and low quantities, laser cutting is usually better. MJM runs both and quotes the most economical route.
Can MJM punch louvers and knockouts?
Yes. Louvers, electrical knockouts, embosses, extrusions, lances and countersink forms are made on the turret punch in the same setup as the holes.
Can I see which punch tools MJM has?
Yes. The full tool library, with sizes, shapes and drawings, is published at mjmmfg.com/tools/.
What materials can be punched?
Mild steel, stainless steel, aluminum, galvanized and galvanneal steel, copper, brass, titanium, polycarbonate and other non-metallic sheet materials.
Related
Related Services
- Turret Punch Tool Library: every punch and forming tool, with drawings.
- Laser Cutting vs CNC Punching: which process fits your part.
- Laser Cutting Services: five Amada lasers, mild steel to 1 in., stainless and aluminum to 5/8 in.
- Precision Forming and Press Brake: nine Amada press brakes to 240 tons and 14 ft.
- Electrical Enclosure Fabrication: NEMA-type boxes, cabinets and panels built to print.
- Custom Metal Fabrication: the full shop under one roof.
- Equipment and Machinery: the full machine list.
Send Us Your Part Files
STEP files and PDF drawings to sales@mjmmfg.com or (305) 620-2020. Quotes in 24 to 48 hours.